Skip to content

Improving industrial sugar mixing safety with a Fristam Powder Mixer & still running perfectly over 15 years after installation.

Fristam Powder Mixer eliminates manual lifting risks while increasing sugar induction speed and operator safety

GET IN TOUCH

Introduction to the application and industry overview

Powder induction into liquid streams is a core process in food and beverage manufacturing, particularly for sugar syrup production. Traditional top-entry batch tank systems often require operators to manually lift and pour heavy bags at height, introducing serious safety risks and inefficiencies. Inline powder mixing technology offers a safer alternative by enabling floor-level operation, controlled induction, and rapid dispersion — improving both workplace safety and production performance.

Customer brief

A large U.S. sucrose processor was producing sugar syrup using a conventional batch tank equipped with a top-entry agitator. Each batch required operators to manually carry 47 bags of 100 lb (45 kg) sugar up a ladder to pour directly into the tank opening.

This repetitive process created a significant safety concern due to heavy lifting, awkward handling positions, and elevated working height. The company sought a safer solution that would eliminate ladder access, reduce physical strain on operators, and improve overall process efficiency.

Previously unsuccessful methods

The existing top-entry mixing process created multiple operational and safety challenges:

  • Operators were required to climb ladders while handling heavy loads
  • Manual pouring increased the risk of slips, falls, and overexertion injuries
  • Batch cycle times were extended due to slow manual addition
  • Ergonomic strain increased fatigue and reduced productivity

These limitations highlighted the need for a floor-level, mechanically assisted powder induction system.

Previously unsuccessful methods

Fristam’s solution

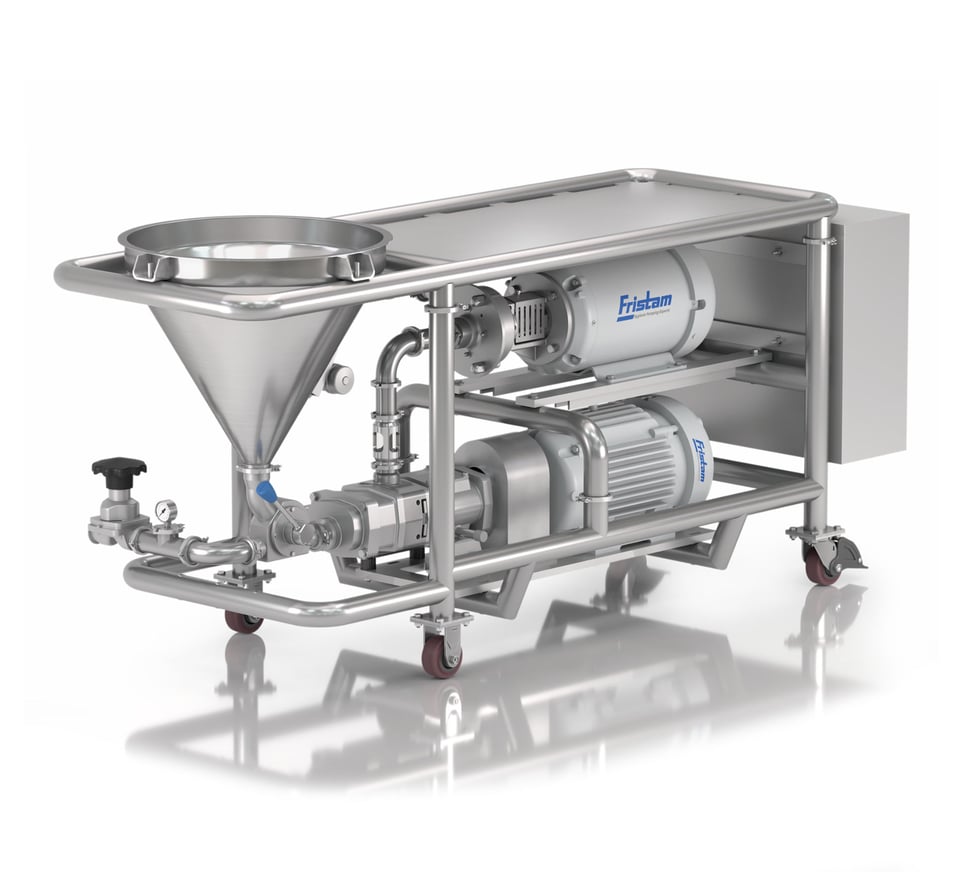
Fristam recommended installing an inline Powder Mixer system as a direct replacement for top-entry powder addition. The solution utilised a high-capacity Liquid Ring Pump to generate vacuum suction for powder induction, combined with inline mixing elements to rapidly disperse sugar into the liquid stream.

The Powder Mixer’s waist-height induction funnel allowed operators to load sugar bags safely at floor level, completely eliminating ladder use. The system was installed adjacent to the existing batch tank and integrated into the circulation loop to maintain continuous, controlled mixing.

For this application, the customer selected a 40-00 USA Powder Mixer, configured to handle high-volume sugar induction while maintaining consistent dispersion and hygienic operation.

Process set-up

1. Floor-level installation
The Powder Mixer was installed beside the batch tank, allowing operators to add sugar safely at ground level.

2. Powder induction operation
Sugar was fed into the Powder Mixer funnel, where vacuum generated by the pump pulled solids directly into the liquid stream.

3. Inline dispersion
As sugar entered the system, inline mixing ensured rapid wet-out and uniform dissolution before returning product to the batch tank.

4. Continuous operation monitoring
Production staff monitored flow rate, induction speed, and operator ergonomics during routine operation to confirm performance improvements.

Fristam’s solution

A successful outcome with the Fristam Powder Mixer

The Powder Mixer immediately transformed the plant’s sugar mixing operation by eliminating the primary safety risk associated with ladder climbing and manual overhead lifting.

Operators were able to load sugar bags at waist height while remaining on the factory floor, significantly improving ergonomics and reducing the risk of workplace injury.

In addition to safety improvements, the Powder Mixer increased sugar induction capacity to approximately 600 lb / 272 kg per minute, reducing batch processing time by around 30 minutes per cycle. This improved overall plant throughput and freed operator time for other production tasks.

More than 15 years after installation, the same Powder Mixer remains in continuous operation — demonstrating long-term reliability and sustained safety benefits.

Do you have any questions so far?

Please don’t hesitate to contact our customer support. We would be happy to answer any questions you may have about our case studies or similar challenges, and we will provide effective solutions tailored to your needs.

Contact us
Process / Product quality benefits

Process / Product quality benefits

  • Uniform and consistent sugar dissolution
  • Stable syrup concentration across batches
  • Reduced batch cycle times
  • Improved repeatability and process control
Sustainability benefits

Sustainability benefits

  • Reduced energy consumption through shorter mixing cycles
  • Less material waste from controlled powder induction
  • Improved resource efficiency through streamlined operations
Financial benefits

Financial benefits

  • Reduced labour requirements per batch
  • Lower indirect costs associated with workplace injury risk
  • Increased production output through faster processing
  • Long equipment service life with minimal maintenance
Other benefits

Other benefits

  • Floor-level ergonomic operation improves health and safety compliance
  • Compact inline installation minimises space requirements
  • Reliable, low-maintenance operation over extended service life

Similar applications

The Fristam Powder Mixer is well suited for:

  • Sugar syrup preparation
  • Beverage sweetener blending
  • Dry ingredient induction for sauces and condiments
  • Powdered stabiliser and gum dispersion
  • Confectionery syrup production
  • Nutritional ingredient dissolution

In addition to Mixing & Blending Technology – check out Fristam’s full range of Pumping Technologies suitable for the Food Industry.

GO TO FRISTAM PUMPS

Share this content