Process / Product quality benefits
- Fully homogeneous, agglomerate-free reconstituted milk
- Reliable suitability for pasteurisation and re-drying
- Consistent recovery of off-spec powder batches
- Standardised process & repeatable recipe
Content on this site is tailored by region. Pick the one that applies to you.
using the Fristam Powder Mixer
GET IN TOUCHIndustrial dairy processors routinely reconstitute dried milk powder to produce standardised liquid milk for further processing, including pasteurisation, blending, fermentation, and spray drying. Reliable milk powder reconstitution is essential to achieve smooth, agglomerate-free liquid milk with consistent solids content, stable functionality and predictable downstream behaviour in dairy manufacturing. It is also a critical process for recovering off-spec powder and returning it to the production cycle as saleable product.
Conventional reconstitution and milk powder mixing methods can be slow, inconsistent, and operationally complex, limiting efficiency in high-throughput dairy environments. This case study demonstrates how a major European dairy ingredient producer used Fristam Powder Mixer technology to achieve rapid milk powder incorporation, complete homogenisation and reconstituted milk suitable for re-pasteurisation and re-drying within an industrial dairy process.
One of Europe’s largest producers of dried milk powder required an effective method to reconstitute milk powder back into liquid milk, particularly to recover batches that were outside specification. The reconstituted milk needed to be free from agglomerates and suitable for further processing, including pasteurisation and re-drying into a high-quality, saleable product.
The customer’s objective was to achieve consistent, efficient, and reliable powder incorporation while simplifying setup and operation.
Before implementing the Fristam solution, the customer reconstituted dried milk powder using conventional in-tank blending.
Powder was added from above into a vessel equipped with a top-entry mixer or internal agitation device, relying on bulk circulation within the tank to disperse and hydrate the powder.
This approach often resulted in slow wetting, floating powder, and the formation of agglomerates that required extended mixing times to resolve and reduced the practicality of recovering off-spec powder batches.
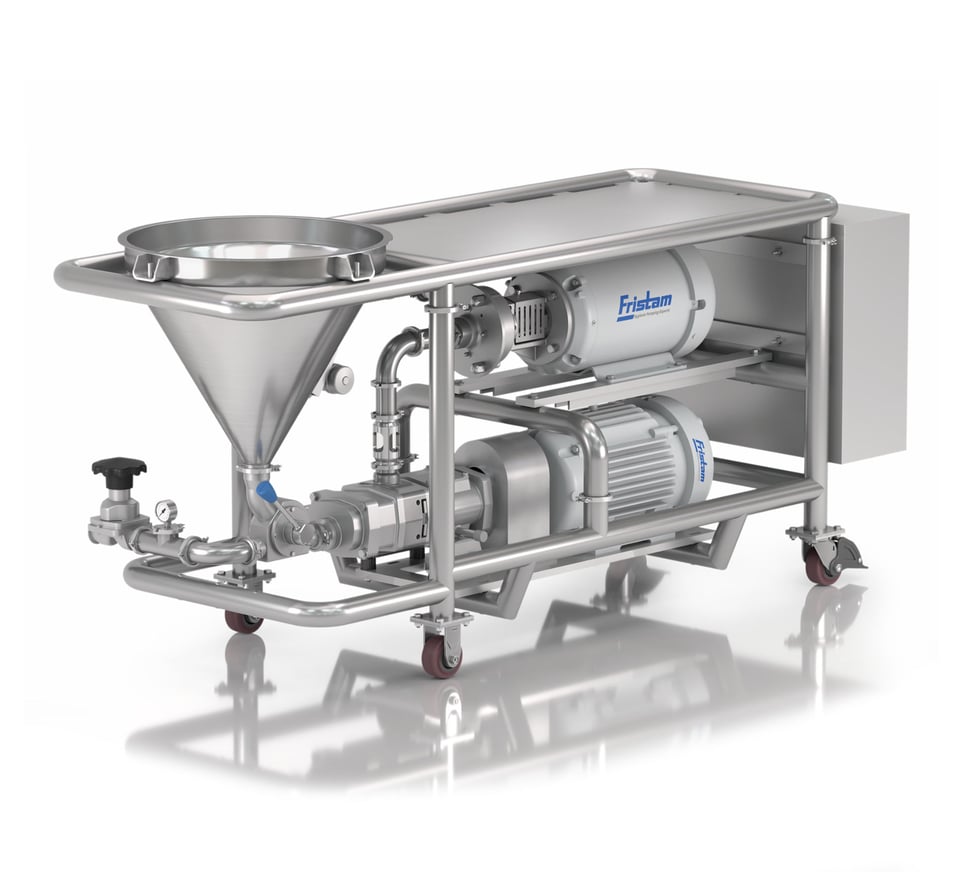
Fristam implemented their PM – a powder-liquid mixing system combining an FZ liquid-ring induction pump with an FS shear blender. This configuration enabled controlled powder induction, rapid dispersion and final homogenisation of dried milk powder directly into water.
The system delivered reliable incorporation rates, simple setup and consistent production of homogeneous reconstituted milk ready for pasteurisation and re-drying.
Trial set up
1. Water was supplied from a 50,000-litre vessel, with suction conditions controlled to maintain stable negative pressure at the mixer inlet.
2. The FZ liquid-ring pump was started to generate vacuum under the mixers hopper.
3. Dried milk powder was introduced via 25 kg bags and drawn into the liquid stream at a rate of approximately one bag per minute. A gentle vibrator attached to the hopper helped the powder flow smoothly downwards.
4. The powder and liquid met under the hopper, where the powders were immediately wetted. This pre-mix was then passed through the FS Shear Blender, which created a fully homogeneous blend of water and milk powder.
5. Mixing continued until a 10:1 liquid-to-powder ratio was achieved, after which the reconstituted milk was sampled for laboratory analysis.
Laboratory analysis confirmed a fully homogeneous reconstituted milk free from agglomerates. The system performed successfully on the first trial, proved simple to set up and operate, and was subsequently adopted by the customer for routine milk powder reconstitution – typically processing around 4,000 kg of powder per batch.
Please don’t hesitate to contact our customer support. We would be happy to answer any questions you may have about our case studies or similar challenges, and we will provide effective solutions tailored to your needs.
Industrial reconstitution of dairy powders such as skimmed milk powder, whole milk powder, whey powder, and milk protein concentrates for use in liquid milk standardisation, yoghurt and cultured product manufacture, ice cream production, and recombined dairy beverages. Powder-into-liquid mixing for nutritional formulations, infant nutrition bases, protein-enriched drinks, and functional dairy ingredients where smooth hydration, full dispersion, and controlled solids content are critical to downstream processing.
Comparable reconstitution and dispersion duties are also found in plant-based dairy alternatives, beverage premixes, bakery and confectionery ingredients, and broader food ingredient processing where powdered raw materials must be efficiently converted into homogeneous liquid phases. In addition, the controlled recovery and reuse of off-spec or surplus powdered products supports yield improvement, waste reduction, and sustainable operation across modern food and dairy manufacturing environments.
Industrial dairies reconstitute milk powder to produce standardised liquid milk for pasteurisation, fermentation, blending, and spray drying. This process also enables recovery of off-spec powder and supports flexible production of dairy ingredients and finished products.
Common issues include poor powder wetting, floating particles, agglomerate formation, long mixing times, and inconsistent solids distribution—especially when using conventional in-tank blending methods. Using a Fristam Powder Mixer ensures these issues do not occur.
Inline mixing draws powder directly into a moving liquid stream and applies controlled shear, enabling rapid hydration, full dispersion, and homogeneous liquid milk with predictable downstream processing behaviour.
The Fristam Powder Mixer combines vacuum powder induction with high-shear homogenisation, allowing fast incorporation of large powder volumes, consistent agglomerate-free mixing and reliable preparation of reconstituted milk ready for pasteurisation or re-drying.
In the referenced application, powder was inducted at approximately one 25 kg bag per minute, enabling efficient processing of large batch quantities and supporting high-throughput dairy production.
Yes. Fully homogeneous reconstituted milk is suitable for downstream operations such as pasteurisation, concentration, fermentation, or spray drying into saleable dairy powder.
A hygienic centrifugal pump such as the Fristam FP is commonly used for low-viscosity dairy liquids, providing gentle, energy-efficient transfer into the powder-mixing system while maintaining product quality.
Rapid, homogeneous mixing reduces energy use, minimises product waste, and enables recovery of off-spec powder – improving raw-material utilisation and overall process efficiency.
Similar processes are used in nutritional beverages, infant formula, protein drinks, plant-based alternatives, bakery and confectionery ingredients, and pharmaceutical or personal-care formulations – anywhere powdered materials must be converted into stable, homogeneous liquids for further manufacturing.