
Process benefits
- Full cocoa powder dispersion in 1 pass, creating a stable, homogenous liquid
- 100% cocoa usage — no settling or waste
- 30% reduction in induction time, improving throughput
Content on this site is tailored by region. Pick the one that applies to you.
Tri-Blender system with batch recirculation:
The processor filled a 4,200 gallon / 15,899 litre tank with milk and recirculated it through a Tri-Blender. Liquid sugar 3,100 lbs / 1,406 kg and cocoa powder 700 lbs / 318 kg were added during the mixing phase.
However, cocoa powder routinely clumped and settled out. After mixing and tank emptying, operators still found roughly 30 lbs / 13.6 kg of undispersed cocoa at the bottom — wasted at a cost of $150 / €139 per batch.
This waste occurred despite using extra cocoa and extended mixing times. The Tri-Blender simply could not achieve the required shear to fully incorporate cocoa powder into the liquid.

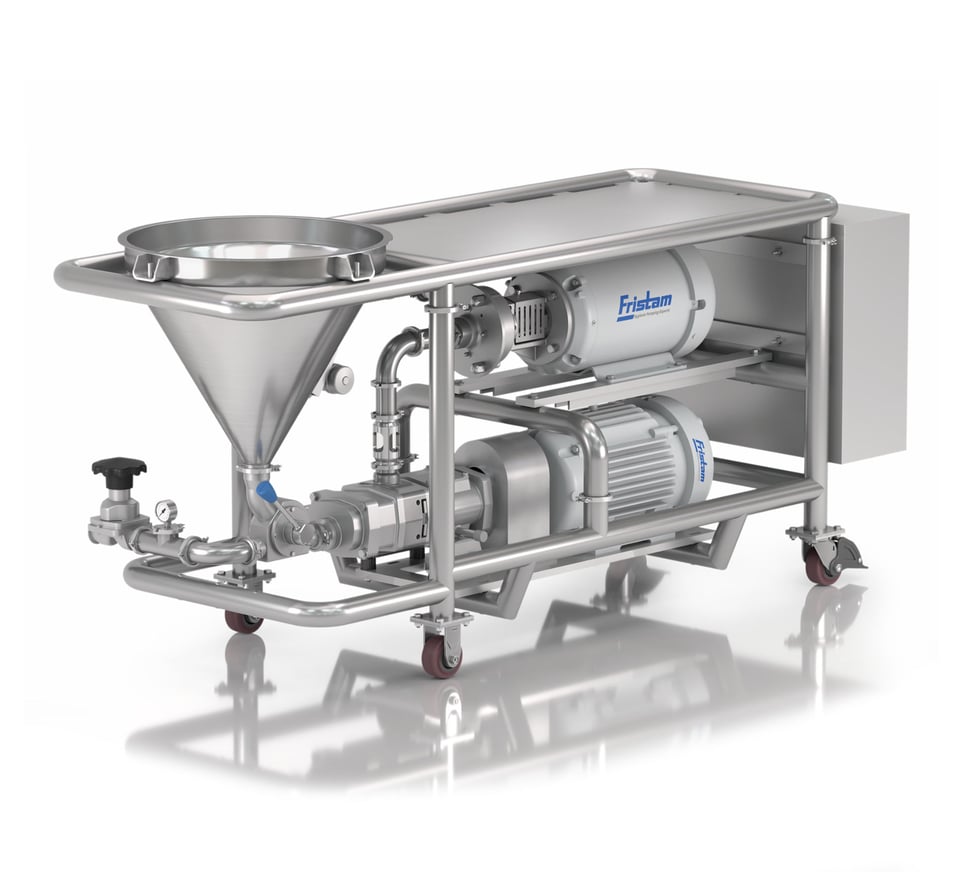
A mid-sized Powder Mixing System.
To ensure the dairy could see real-world performance before purchase, a live on-site trial was arranged using the Fristam Powder Mixer. The dairy followed their original process sequence: milk recirculation, addition of liquid sugar, followed by cocoa powder.
Process overview
1. Trial set-up
The Fristam Powder Mixer was integrated into the existing batch mixing line. The product was set to recirculate continuously from the tank base to the top.
2. Controlled cocoa powder induction
Cocoa powder was steadily poured into the funnel. The induction pump below generated vacuum and flow, pulling powder into the liquid stream at a controlled rate — preventing clumping and ensuring stable dispersion.
3. High-shear mixing
The mixture passed through Fristam’s FS Shear Blender, where high tip speeds and narrow clearances produced intense shear forces. This dispersed cocoa evenly into the milk, forming a homogenous chocolate milk blend in one circulation.


The Fristam Powder Mixer delivered full cocoa powder dispersion, eliminating tank residue and reducing ingredient usage. The processor continued producing three batches per day. By saving 30 lbs / 13.6 kg of cocoa per batch, valued at $150 / €139, they achieved:
With the cocoa dissolving in a single pass, there was no need for extended recirculation or overuse of cocoa, the system paid for itself in a short period while enhancing product consistency.


